Milling a waterproof luxury watch case and integrated bracelet from a solid forged 18K gold (Au750) billet requires simultaneous 5-axis Swiss CNC machining centers (such as Willemin-Macodel 408MT) operating at 42,000 RPM with monocrystalline diamond (MCD) cutters to hold ±0.002 mm (2-micron) gasket-seat tolerances and crisp architectural bevels.
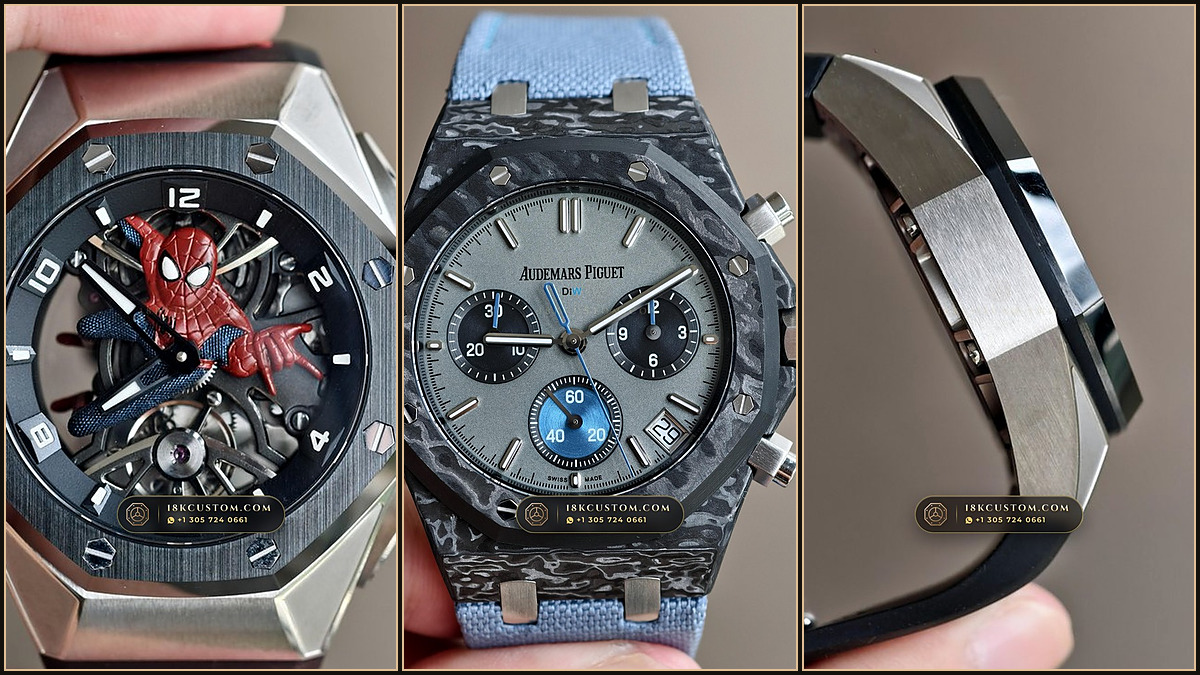
Key Quantitative Laboratory Takeaways
- Starting from a 650-gram forged solid 18K gold billet, over 75% of the gold mass is milled away as swarf (and recycled in-house) to produce a single 95-gram finished monobloc middle case and bezel.
- Simultaneous 5-axis kinematic interpolation allows the diamond cutter to machine compound undercuts, crown-guard scallops, and integrated lug chamfers in a single clamping setup with zero datum shift.
- Crystal gasket shoulders, Triplock/Twinlock crown tube threads, and caseback sealing grooves are held to ±0.002 mm (2 microns) so every bespoke build passes 5 ATM to 10 ATM Witschi Proofs.
- Monocrystalline diamond (MCD) finishing tools produce a sub-0.02 um Ra mirror surface directly off the spindle prior to manual gentian-wood anglage.
| Case Engineering Zone | Target Dimensional Tolerance | Surface Roughness (Ra) | Cutting Tooling Used | Functional Impact |
|---|---|---|---|---|
| Sapphire Crystal Seat | +/- 0.002 mm (2 Microns) | Ra <= 0.08 um | PCD Micro-Boring Head | Prevents crystal tilt & ensures 100m waterproof seal |
| Movement Casing Ring Bore | +/- 0.003 mm (3 Microns) | Ra <= 0.12 um | Carbide End-Mill (42k RPM) | Eliminates stem misalignment & rotor rub |
| Crown & Pusher Tube Threads | ISO Metric Pitch +/- 0.002 mm | Ra <= 0.10 um | Single-Point Diamond Threader | Buttery screw-down crown & pusher engagement |
| Octagonal Bezel Chamfers | +/- 0.005 mm Angularity | Ra <= 0.015 um (Mirror) | Monocrystalline Diamond (MCD) | Crisp light transition between brushed & polished |
| Bracelet Link Pin Bores | +/- 0.002 mm Concentricity | Ra <= 0.06 um | Deep-Hole Carbide Reamer | Silk-smooth bracelet drape with zero lateral play |
Why 3-Axis CNC Fails and Simultaneous 5-Axis Milling Succeeds on Luxury Cases
A conventional 3-axis milling machine can only move its cutter along the X, Y, and Z linear axes, forcing the operator to unclamp and re-fixture a watch case six to eight times to machine the top lug hoods, side flanks, crown tube bore, and underside hallmark pads. Every re-clamping introduces a 15-to-30-micron alignment error that rounds off the crisp meeting point where three bevels intersect on an Audemars Piguet Royal Oak or Patek Philippe Nautilus case.
At 18K Custom Atelier Geneve, our 5-axis machining centers tilt and rotate the solid 18K gold billet along the B and C rotary axes simultaneously while the spindle runs at 42,000 RPM, machining all exterior geometry, thread bores, and lug chamfers in one continuous datum setup.
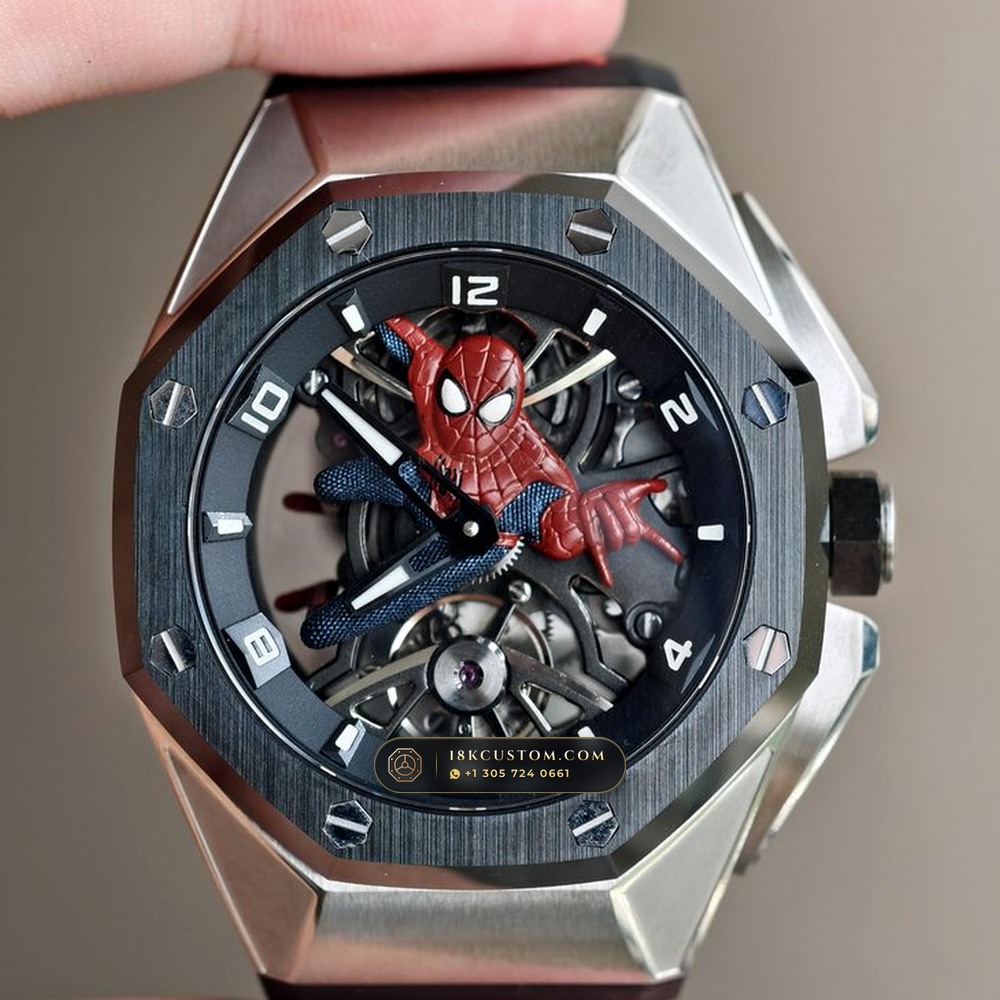
Monocrystalline Diamond (MCD) Tooling on Work-Hardened Au750 Gold
Because 18-karat gold is a gummy, high-ductility noble metal, ordinary tungsten-carbide end-mills suffer from built-up edge (BUE) welding when cutting intricate bevels, tearing microscopic grooves into the surface. For final finishing passes on our fluted Day-Date bezels, octagonal Royal Oak chamfers, and Daytona lug flanks, we utilize natural Monocrystalline Diamond (MCD) tools lapped to a nanometer-sharp cutting edge, producing an optical mirror finish directly on the CNC machine before our polishers apply the final hand-drawn satin brush lines.
| Component Assembly | Raw Au750 Billet Weight | Finished Component Mass | CNC Swarf Recycled (%) | 5-Axis Milling Cycle Time |
|---|---|---|---|---|
| Monobloc Middle Case (40–41mm) | 380.0g Solid Au750 Puck | 54.5g – 62.0g Finished | 84.5% Recycled in Foundry | 14.5 Hours (Rough + MCD Finish) |
| Octagonal / Fluted 18K Bezel | 145.0g Solid Au750 Ring | 22.0g – 26.5g Finished | 82.8% Recycled in Foundry | 8.0 Hours (Diamond Faceting) |
| Threaded / Sapphire Caseback | 110.0g Solid Au750 Disc | 16.5g – 21.0g Finished | 81.5% Recycled in Foundry | 5.5 Hours (Fluting + Hallmarks) |
| Full Integrated 18K Bracelet | 620.0g Solid Au750 Bar | 112.0g – 126.0g Finished | 80.6% Recycled in Foundry | 38.0 Hours (140+ Link Surfaces) |
Holding ±2-Micron Gasket Tolerances for 100-Meter Hydrostatic Pressure Testing
A custom solid 18K gold watch case is only worthy of daily wear if it seals hermetically against moisture and atmospheric pressure changes. By holding the Hytrel crystal gasket seat and Viton caseback O-ring grooves to ±0.002 mm (2 microns), every custom build passes dry vacuum deformation testing and wet hydrostatic pressure testing on our Witschi Proofmaster prior to 4K client video sign-off.
Explore Verified Audemars Piguet Solid 18K Gold References in Our Register
Every timepiece referenced in this monograph is available for immediate allocation with pre-shipment 4K Mettler-Toledo gram weighing, Fischer XRF Au750 spectroscopy, and 6-position Witschi Chronoscope certification. Navigate directly to the 18K CUSTOM Homepage Master Register, the Audemars Piguet Solid 18K Gold Collection Hub, or the Complete 774-Watch Catalogue:
Master Micro-Mechanical Engineer (HES-SO Geneva), 19 Years in Swiss 5-Axis Watch Case & Skeleton Bridge Fabrication.
More Horological Monographs in the 18K CUSTOM Journal
- Authentic Namibian Gibeon & Muonionalusta Meteorite Watch Dials: Wire-EDM Slicing, Nitric Acid Widmanstatten Etching & Rhodium Sealing (September 6, 2026)
- The Art of Hand-Chamfered Openworked Skeleton Bridges: Interior Angles (Angles Rentrants), Gentian-Wood Polishing & Rhodium Plating (September 21, 2026)
- Bespoke Horological Upgrades: Custom SW Natural Stone & Sunburst Dials, Solid 18K Diamond-Cut Hands & Double-AR Deep Sapphire Crystals (October 5, 2026)
- Microscopic Channel & Snow Pave Gem-Setting in Solid 18K Gold: VVS Baguette Diamonds, Blue Topaz, Emeralds & Rainbow Sapphires (October 17, 2026)
- View All 18K CUSTOM Research Journal Articles →